Industrial Process Water
Our cutting-edge technologies are designed to efficiently treat process water, removing impurities and contaminants to meet stringent quality standards.
Overview
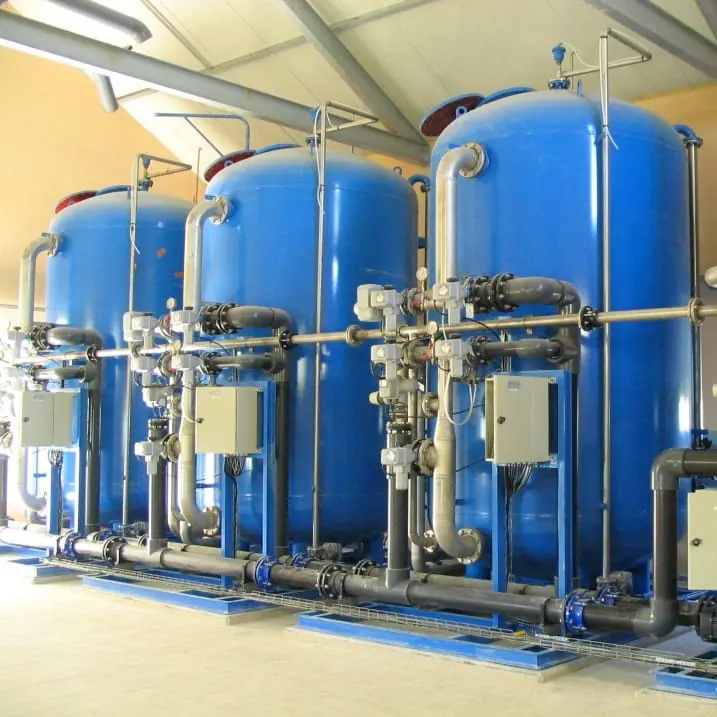
Process water treatment and recycling are paramount for optimizing industrial operations and reducing environmental footprint. Our cutting-edge technologies are designed to efficiently treat process water, removing impurities and contaminants to meet stringent quality standards. By implementing advanced filtration, reverse osmosis, and other specialized techniques, we ensure that process water is purified for reuse in various manufacturing processes, minimizing water consumption and waste generation.
From boiler feed and cooling water make-up to product, rinse and wash water, we design treatment trains matched to each point of use — combining clarification, softening, ion exchange and membrane technologies with high-recovery options such as Closed Circuit Reverse Osmosis and Selective Contaminant Removal to cut water intake, chemical consumption and discharge volumes.
How it works
Treatment train
-
 01
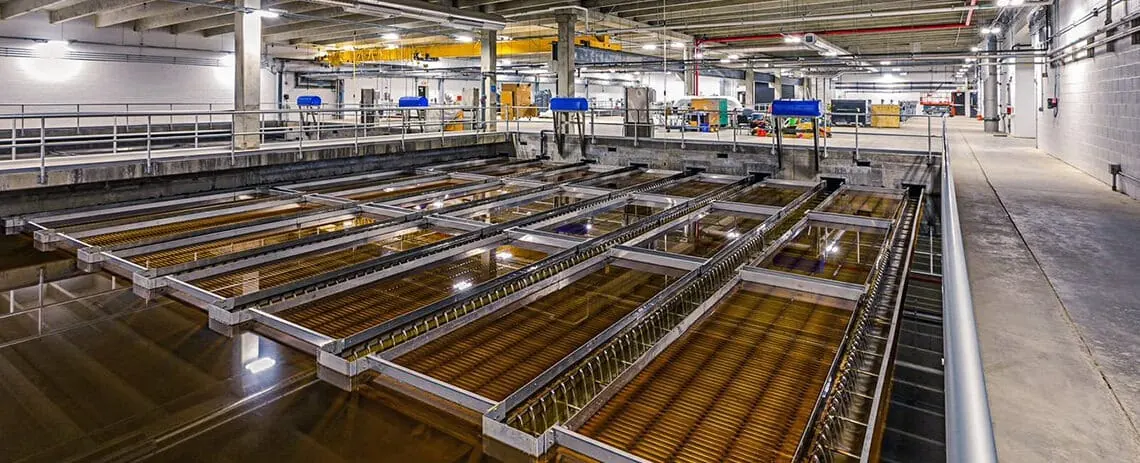
Clarification
Coagulation, flocculation and settling or flotation remove turbidity, suspended solids and colloids from the raw water.
-
 02
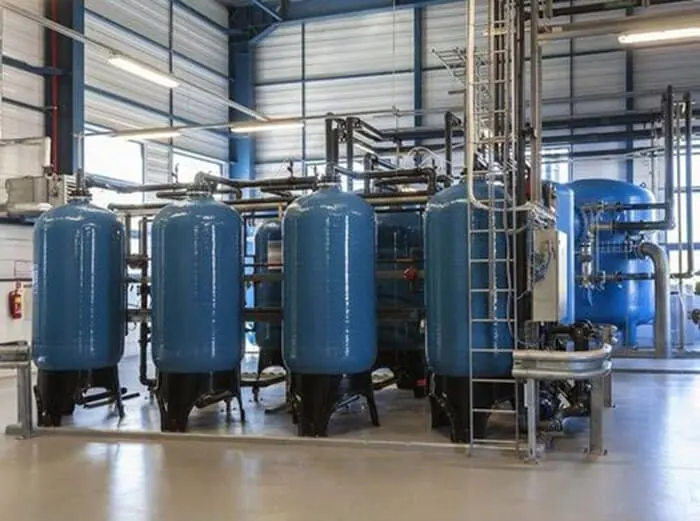
Softening
Softening removes calcium and magnesium hardness to prevent scaling in boilers, cooling circuits and process equipment.
-
 03
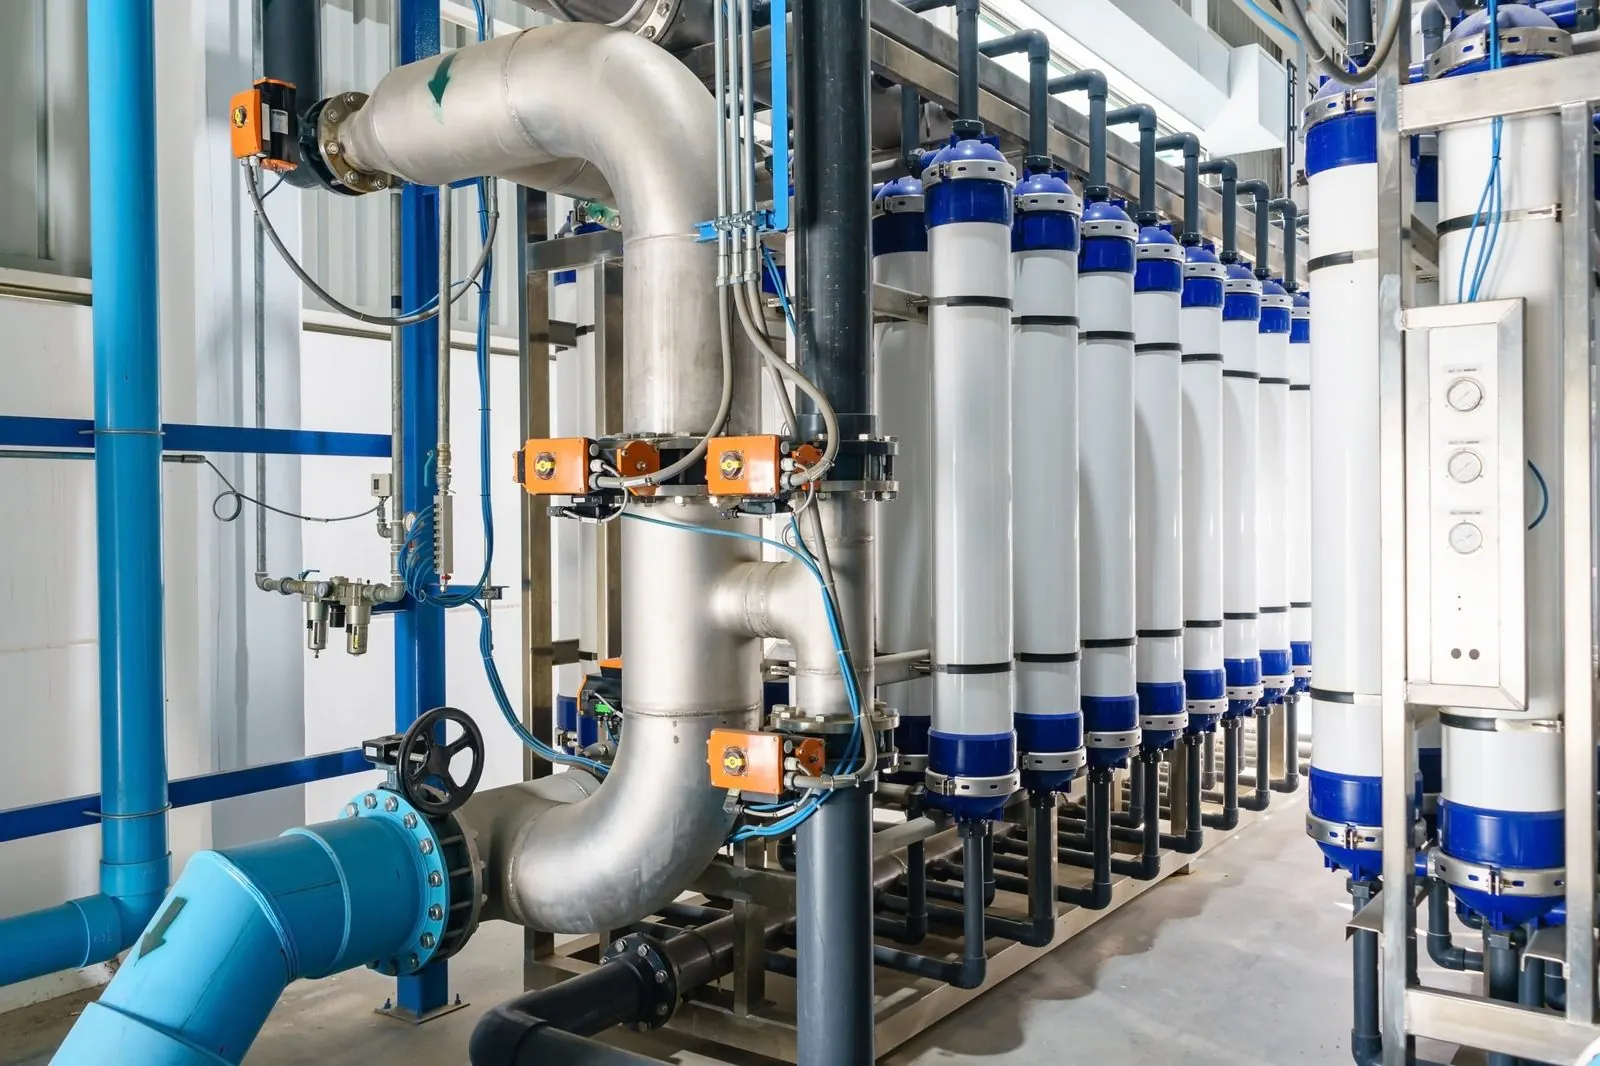
Membrane Technologies
Ultrafiltration and reverse osmosis remove the remaining particles, bacteria and dissolved salts.
-
 04
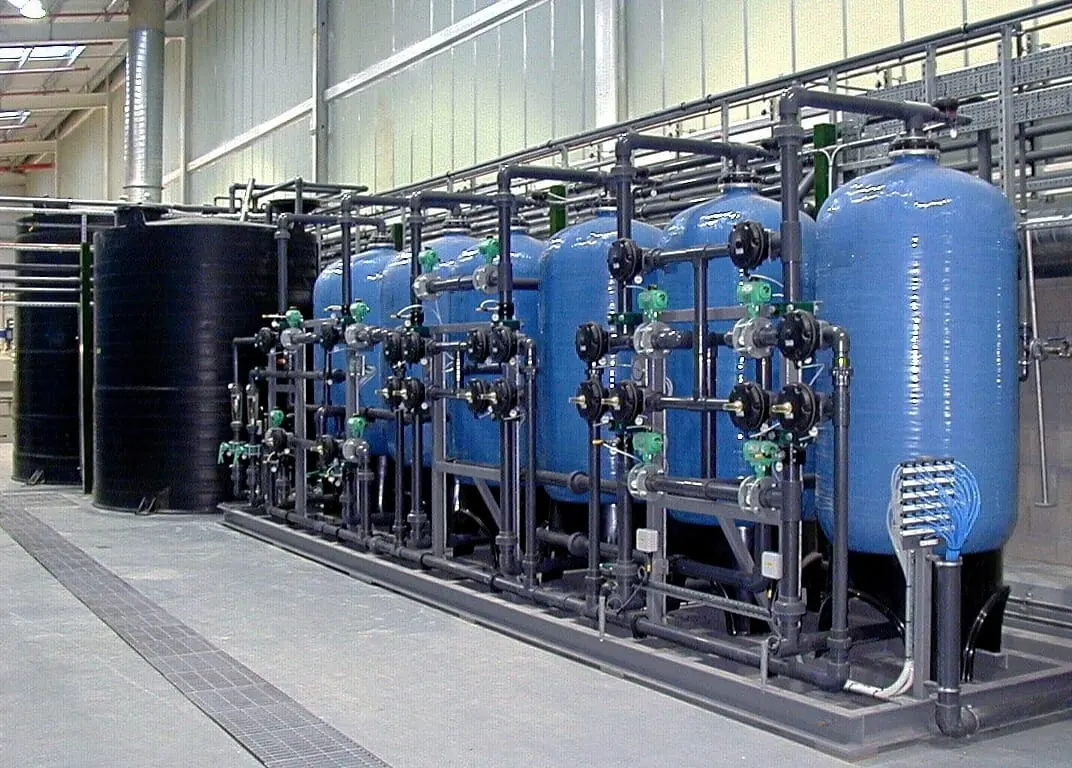
Ion Exchange
Demineralization and mixed-bed polishing deliver the very low conductivity required for boiler feed and sensitive processes.
Technologies
Technologies we apply
Each project combines the processes best suited to the water, the target quality and the site.
Let’s work together
Sustainable water & energy for the future — starting with your project.
From consulting and strategy development to implementation and support, our team is ready to offer the most efficient solution for your site.